Welcome to BJY
Product / OEM Machinery parts / BJY 57 × 275.37 mm Mold Core
BJY 57 × 275.37 mm Mold Core

BJY 57 × 275.37 mm Mold Core

Product Introduction

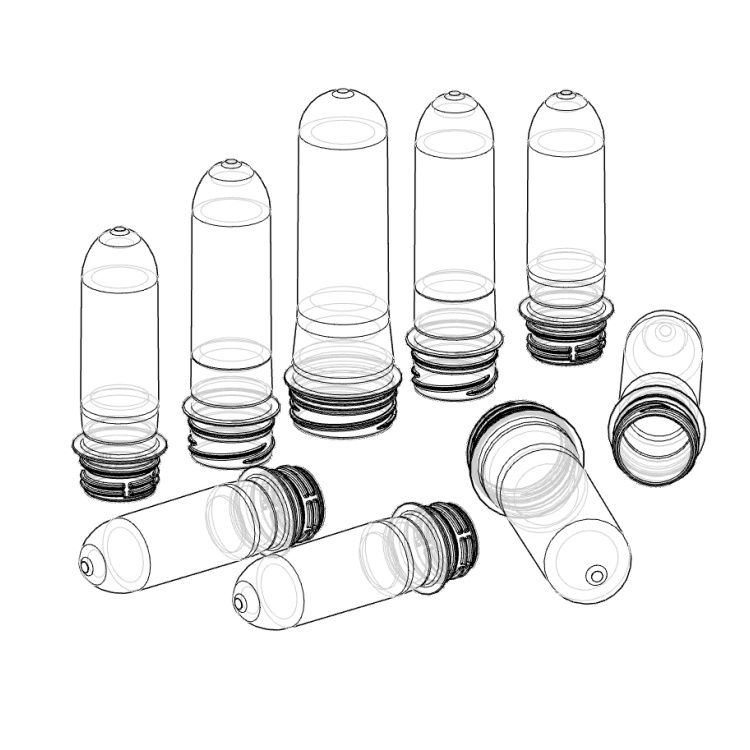
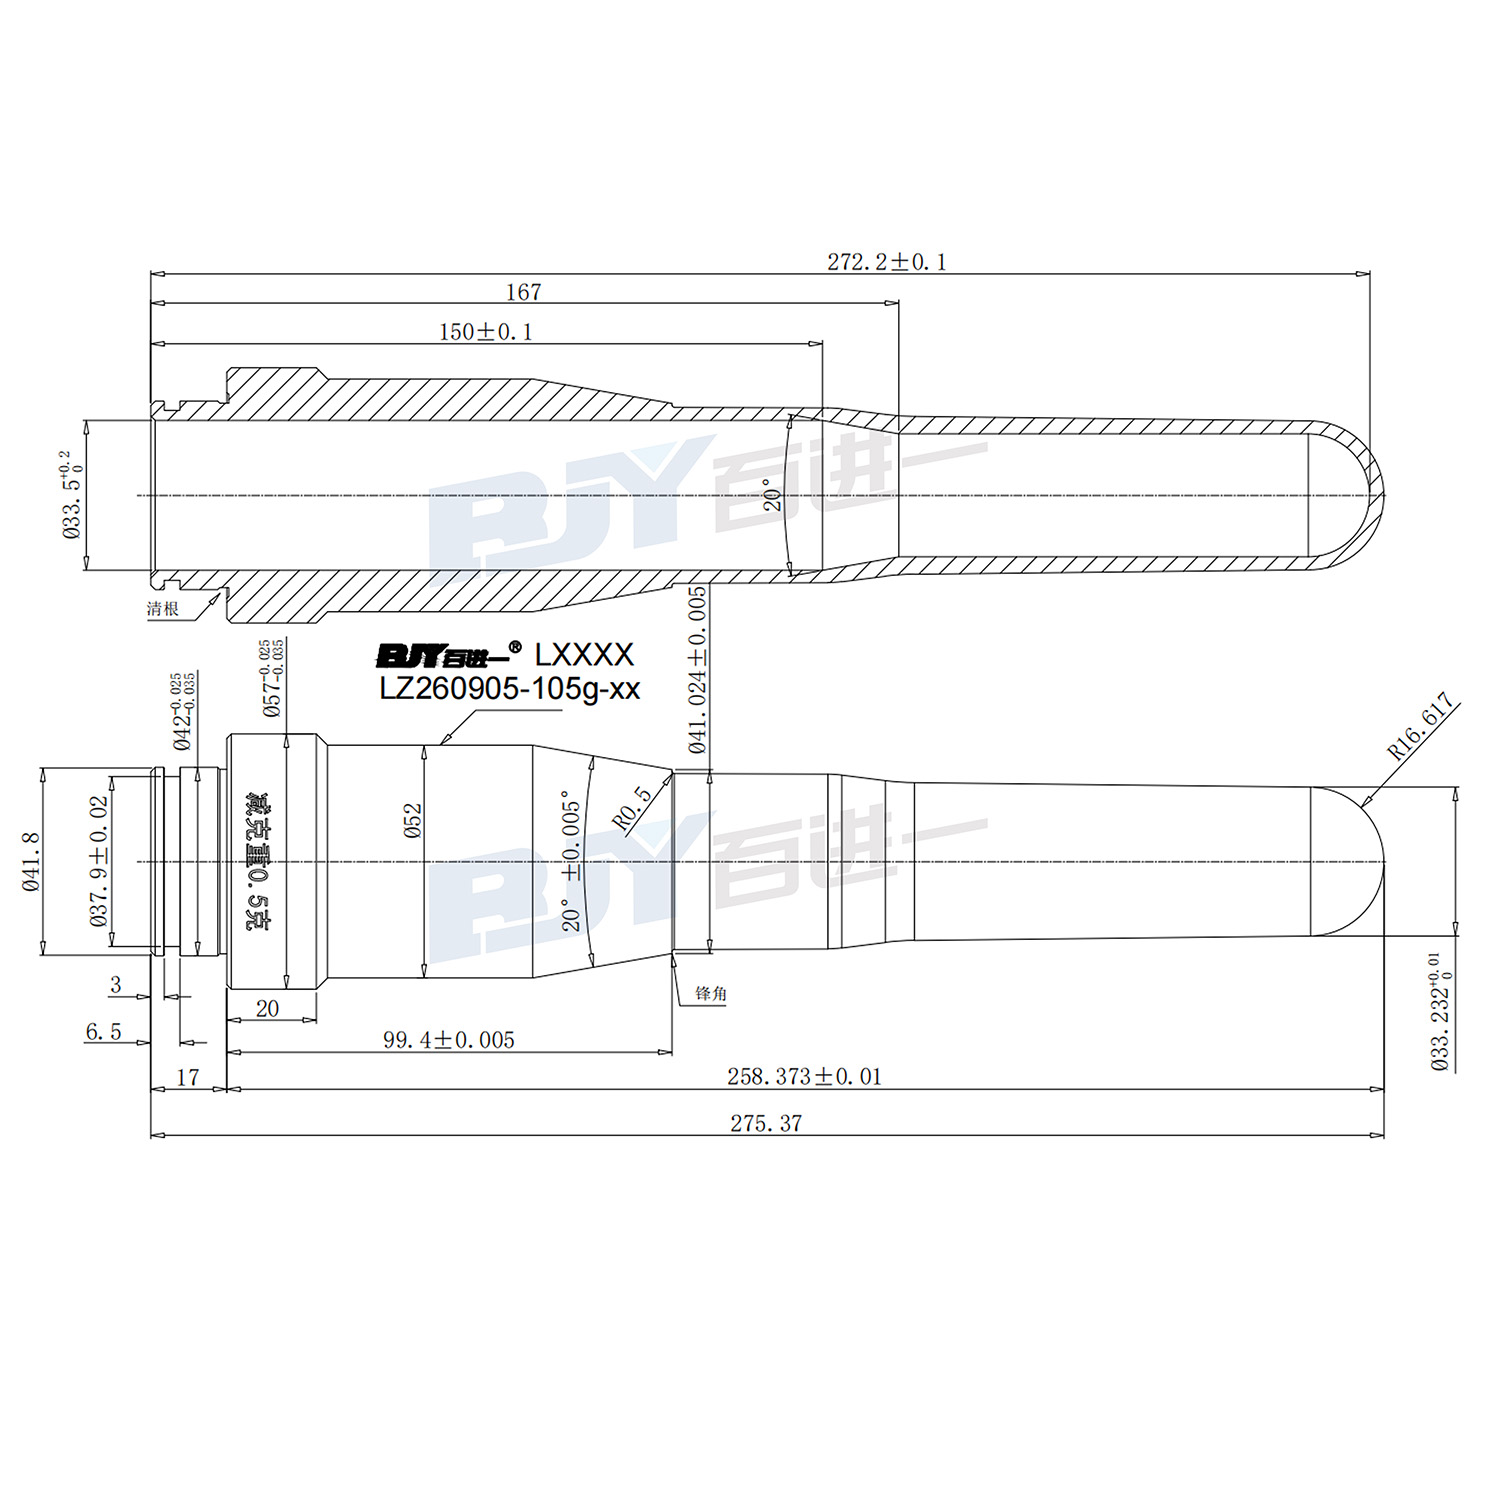
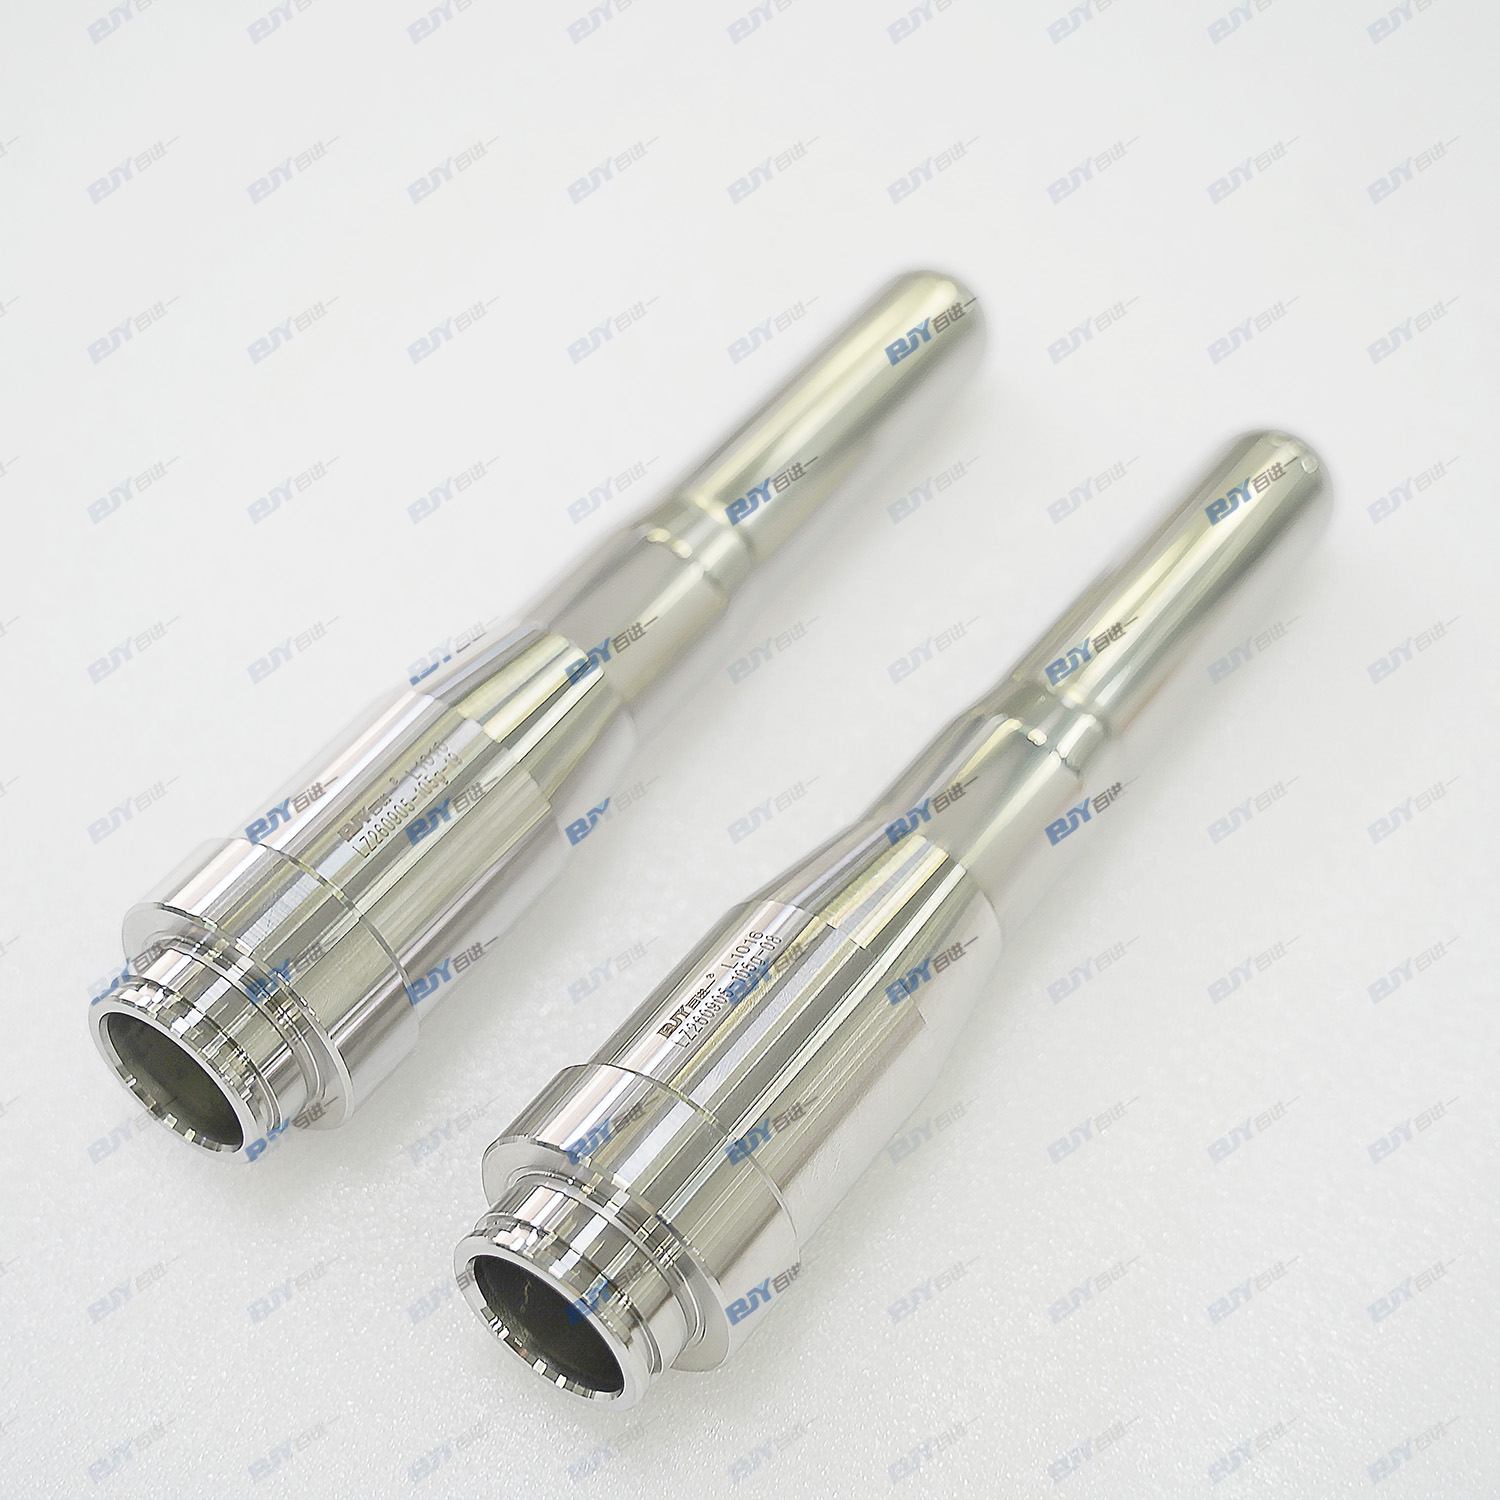
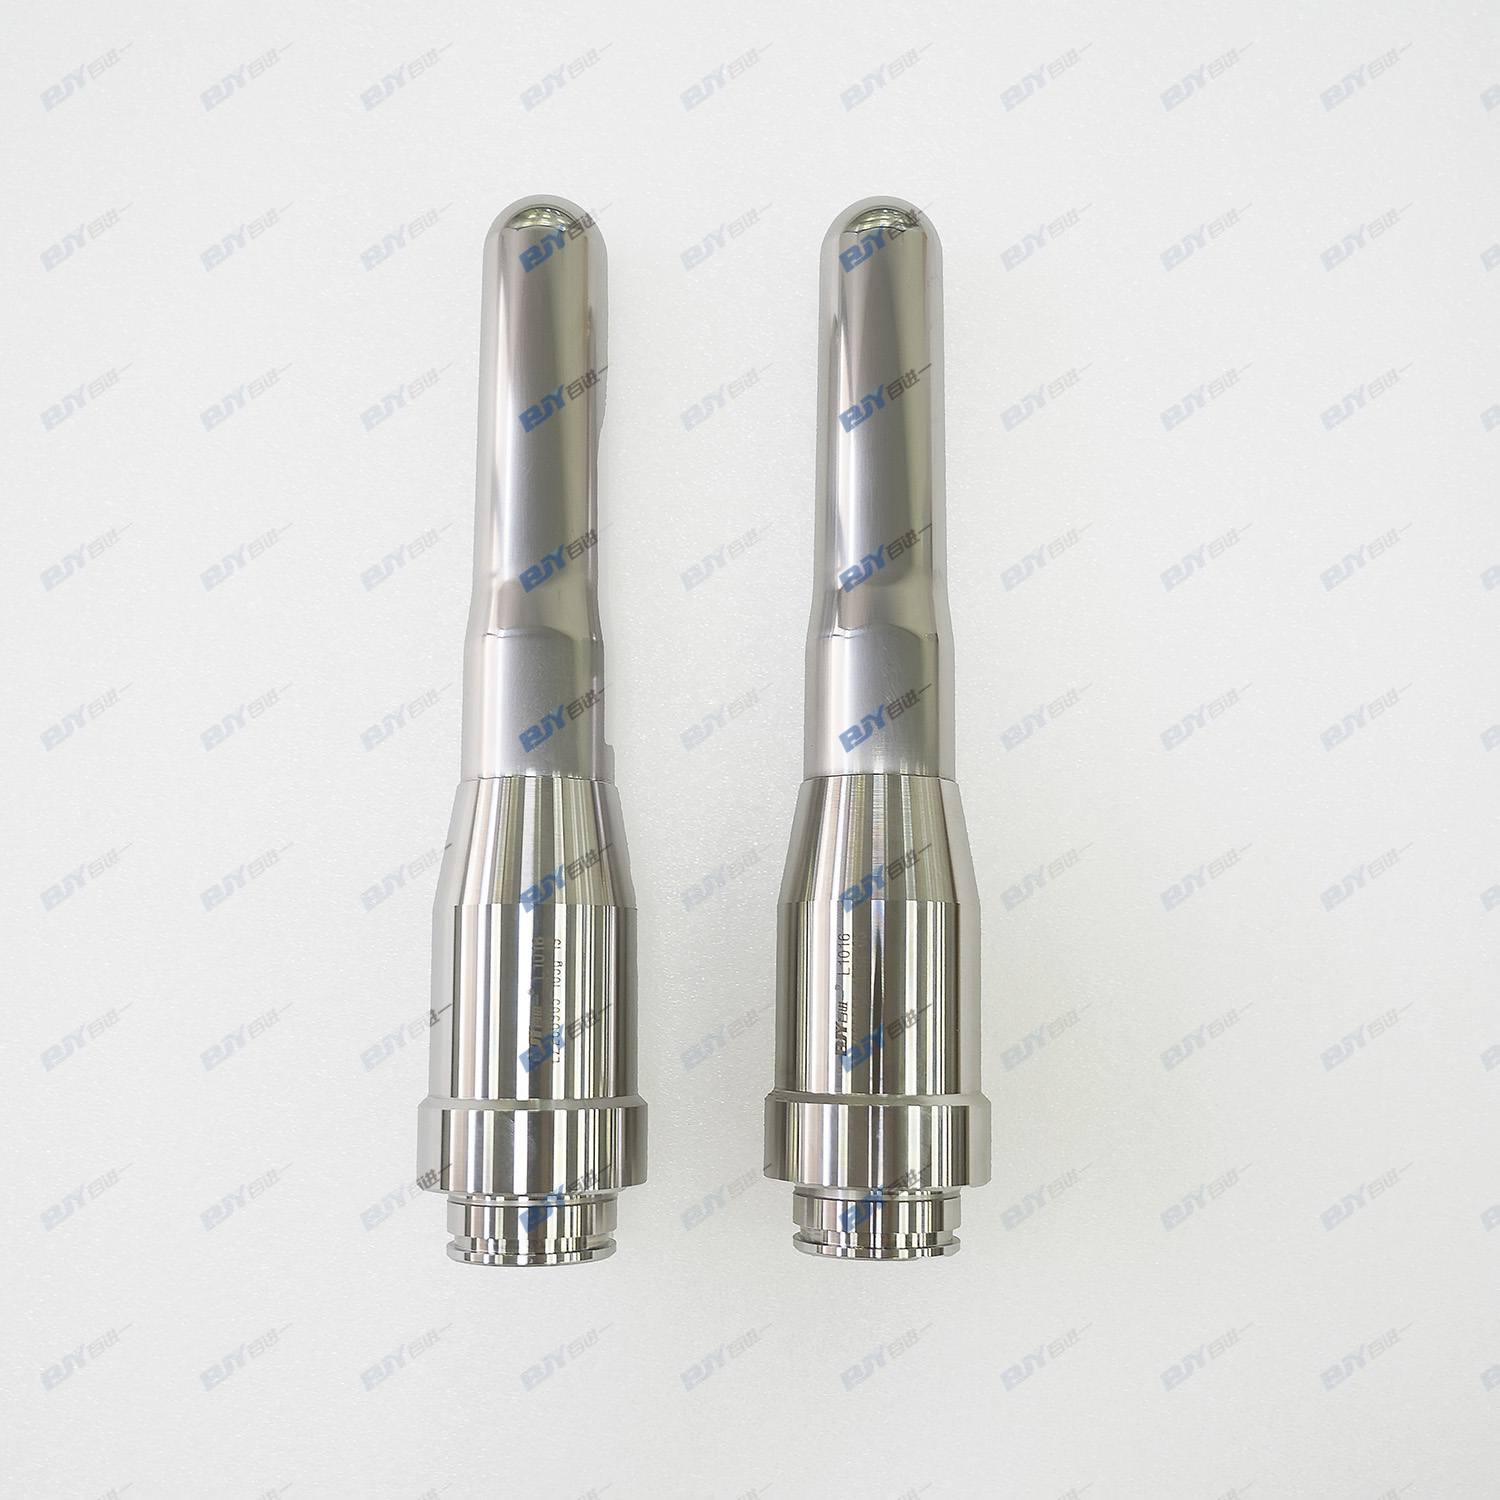
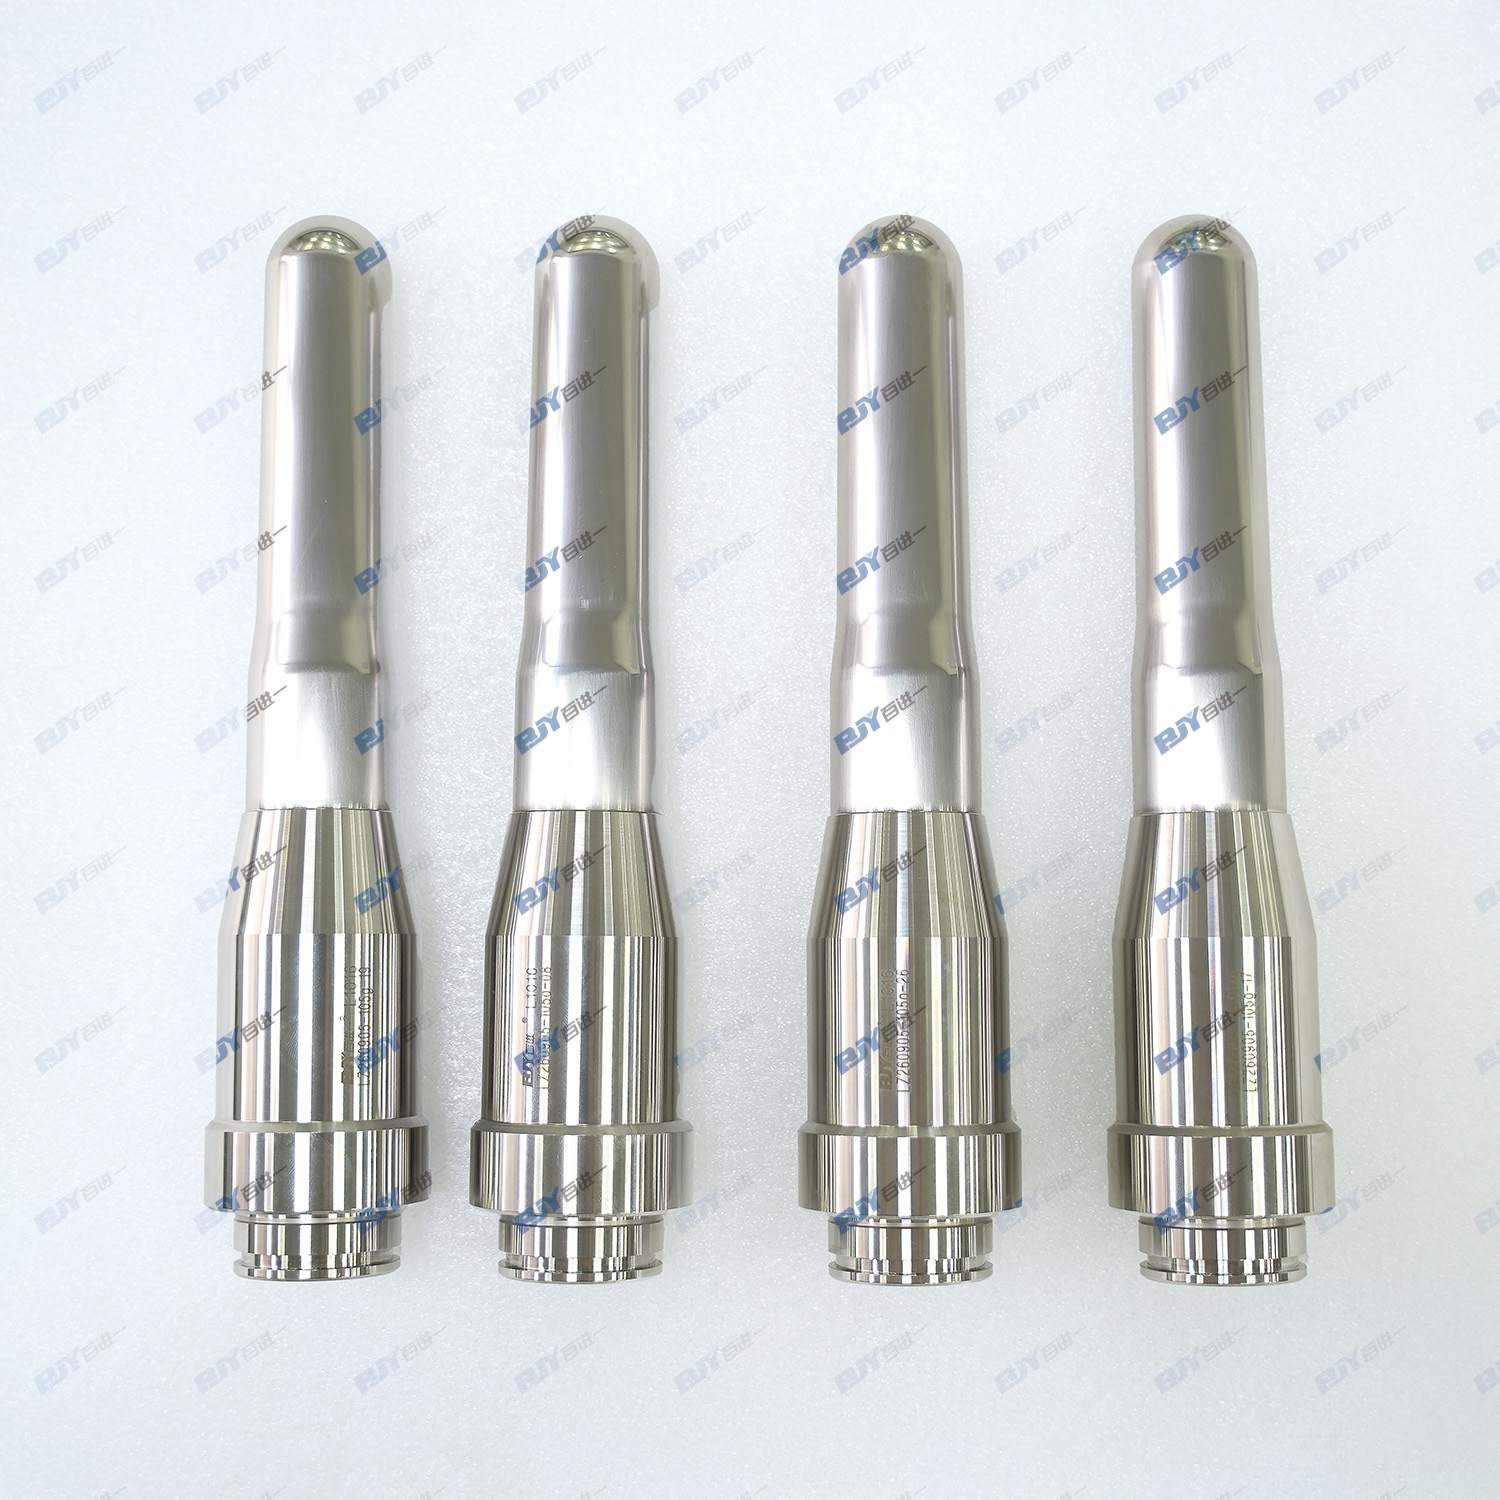
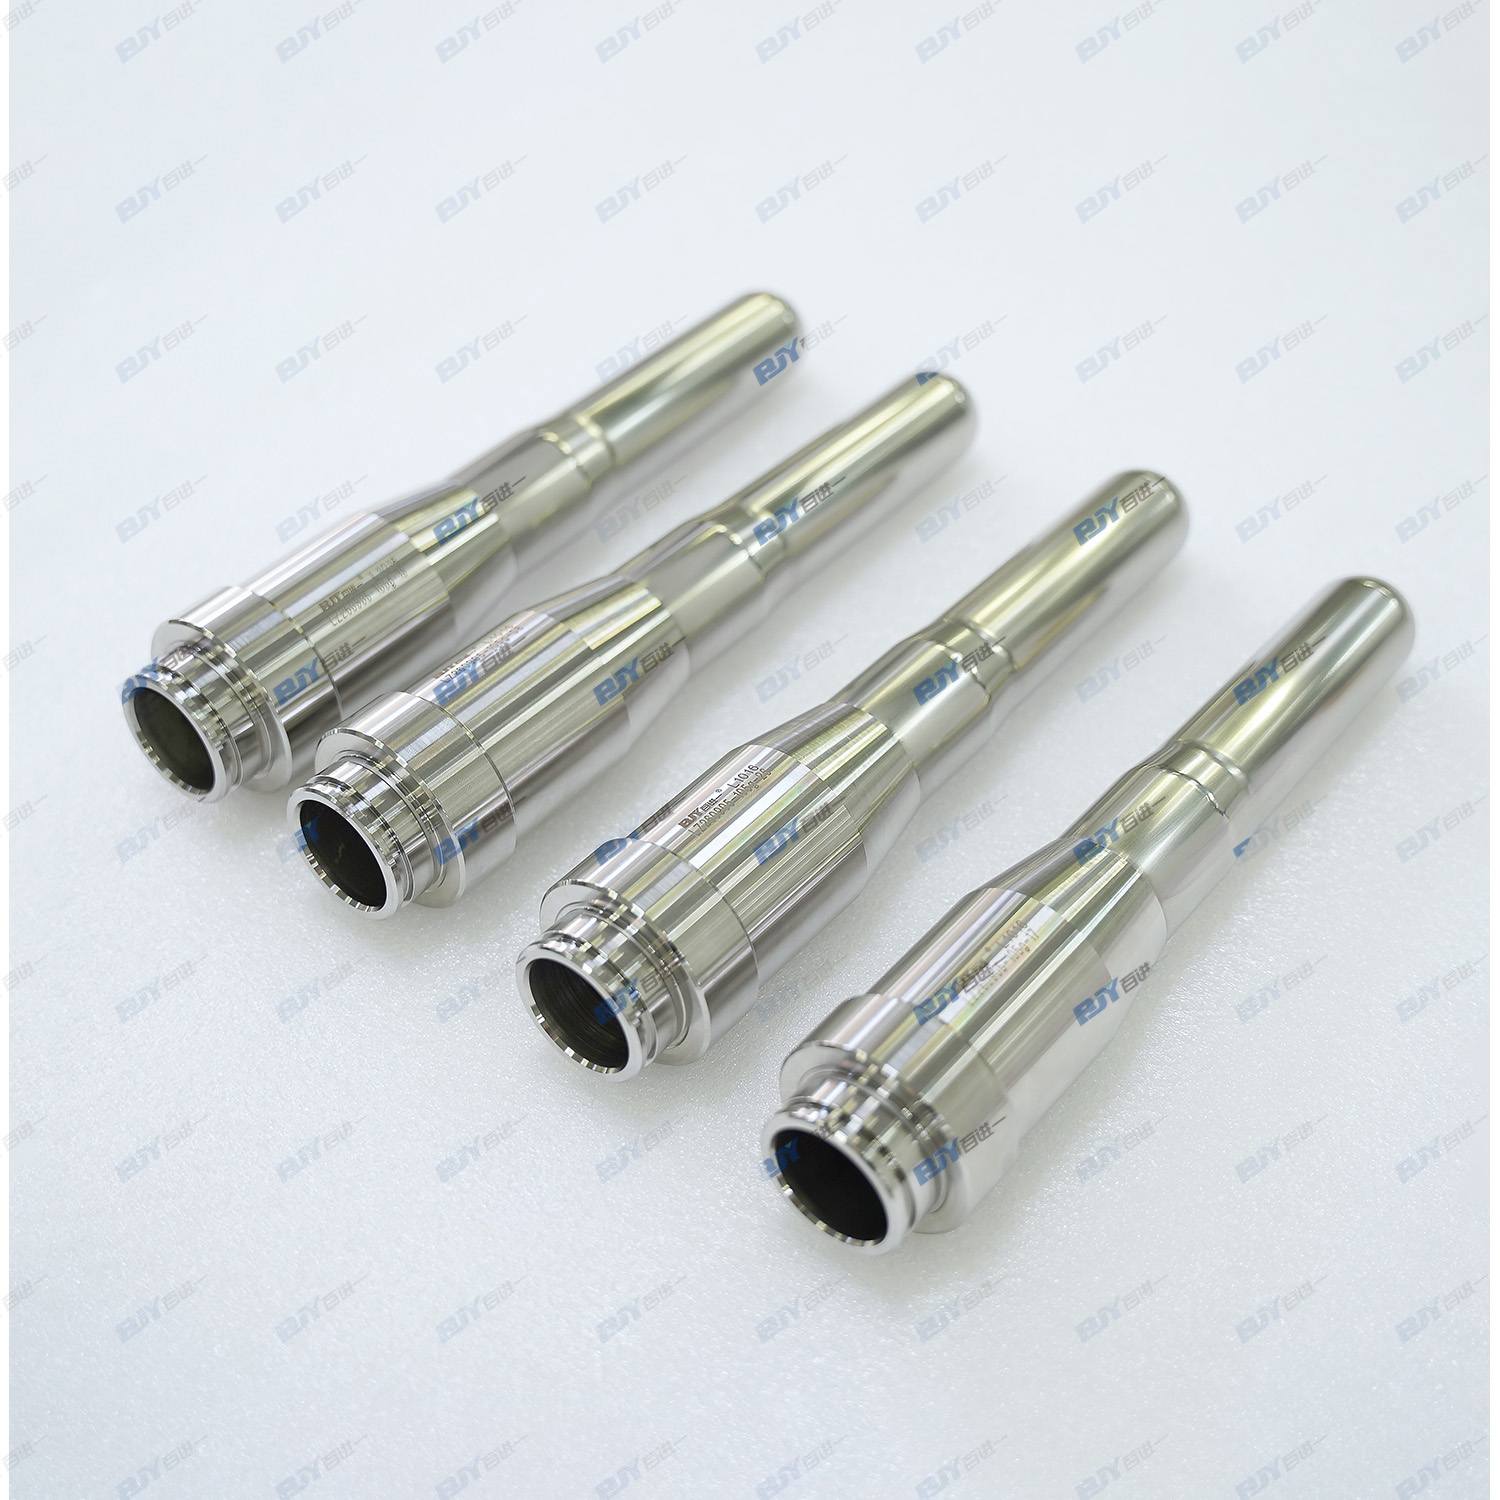
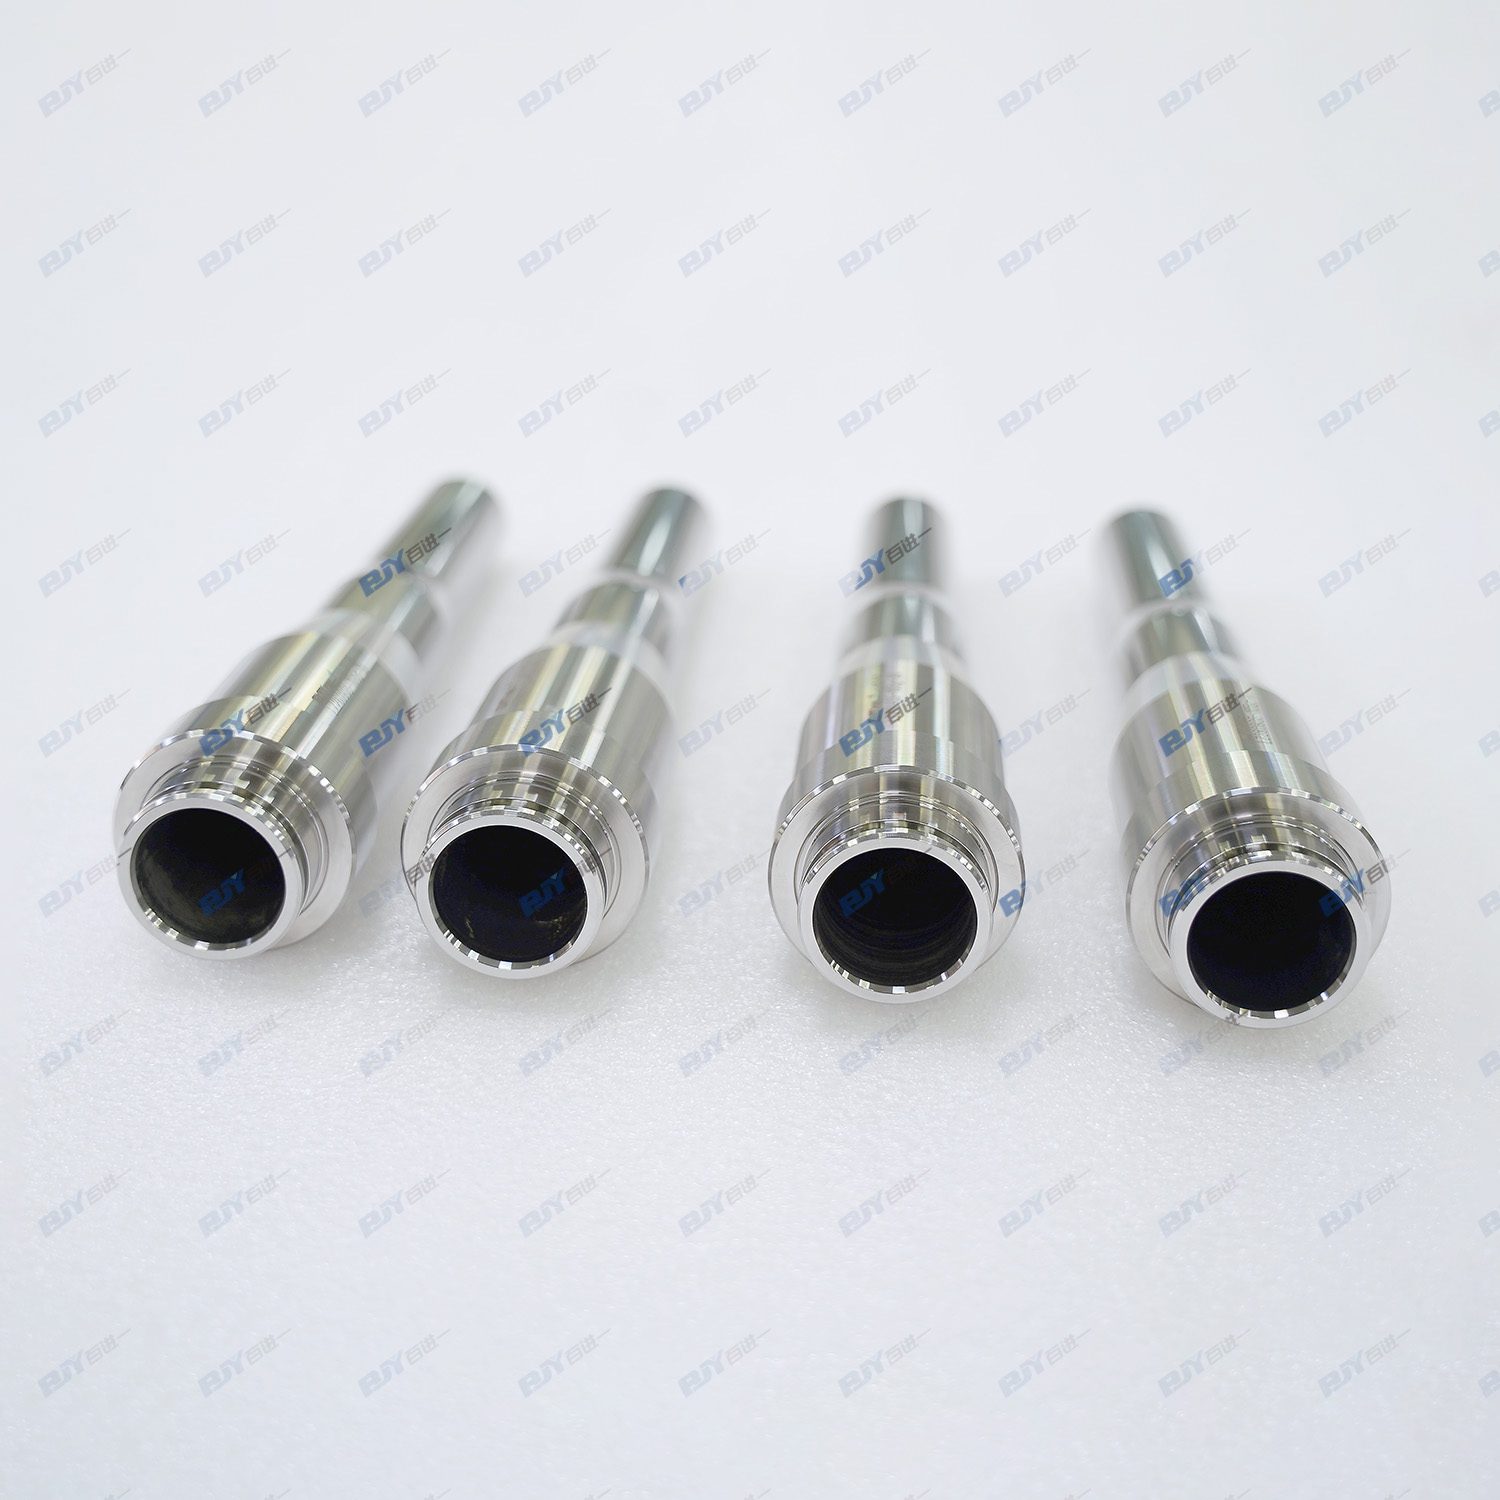
BJY supplies the 57 mm by 275.37 mm mold core for PET preform injection molds. The core forms the inner wall of the preform body: the shoulder, the side wall and the base. It is mounted in the core seat of the mold, and a water core runs with the assembly to carry heat out during every shot.


Product Details

Item

Detail

Product Name

Mold Core (PET Preform Mold)

Size

Ø57 mm × 275.37 mm (diameter × overall length)

Machining

Precision machining per customer drawing and preform layout

Inspection

Straightnes and concentricity measured after machining; dimensional record filed with every lot

Spare Parts

Replacement cores cut from the same drawing and inspection record

Application

PET preform lines of beverage plants

Customization

Made to customer drawing for other preform sizes


BJY supplies mold cores in the 57 mm by 275.37 mm configuration for PET preform lines. The mold core is installed inside the injection molding mold.
  • pet-preform-mold-core-concentricity-inspection.jpg

    One Shot, Complete Inside

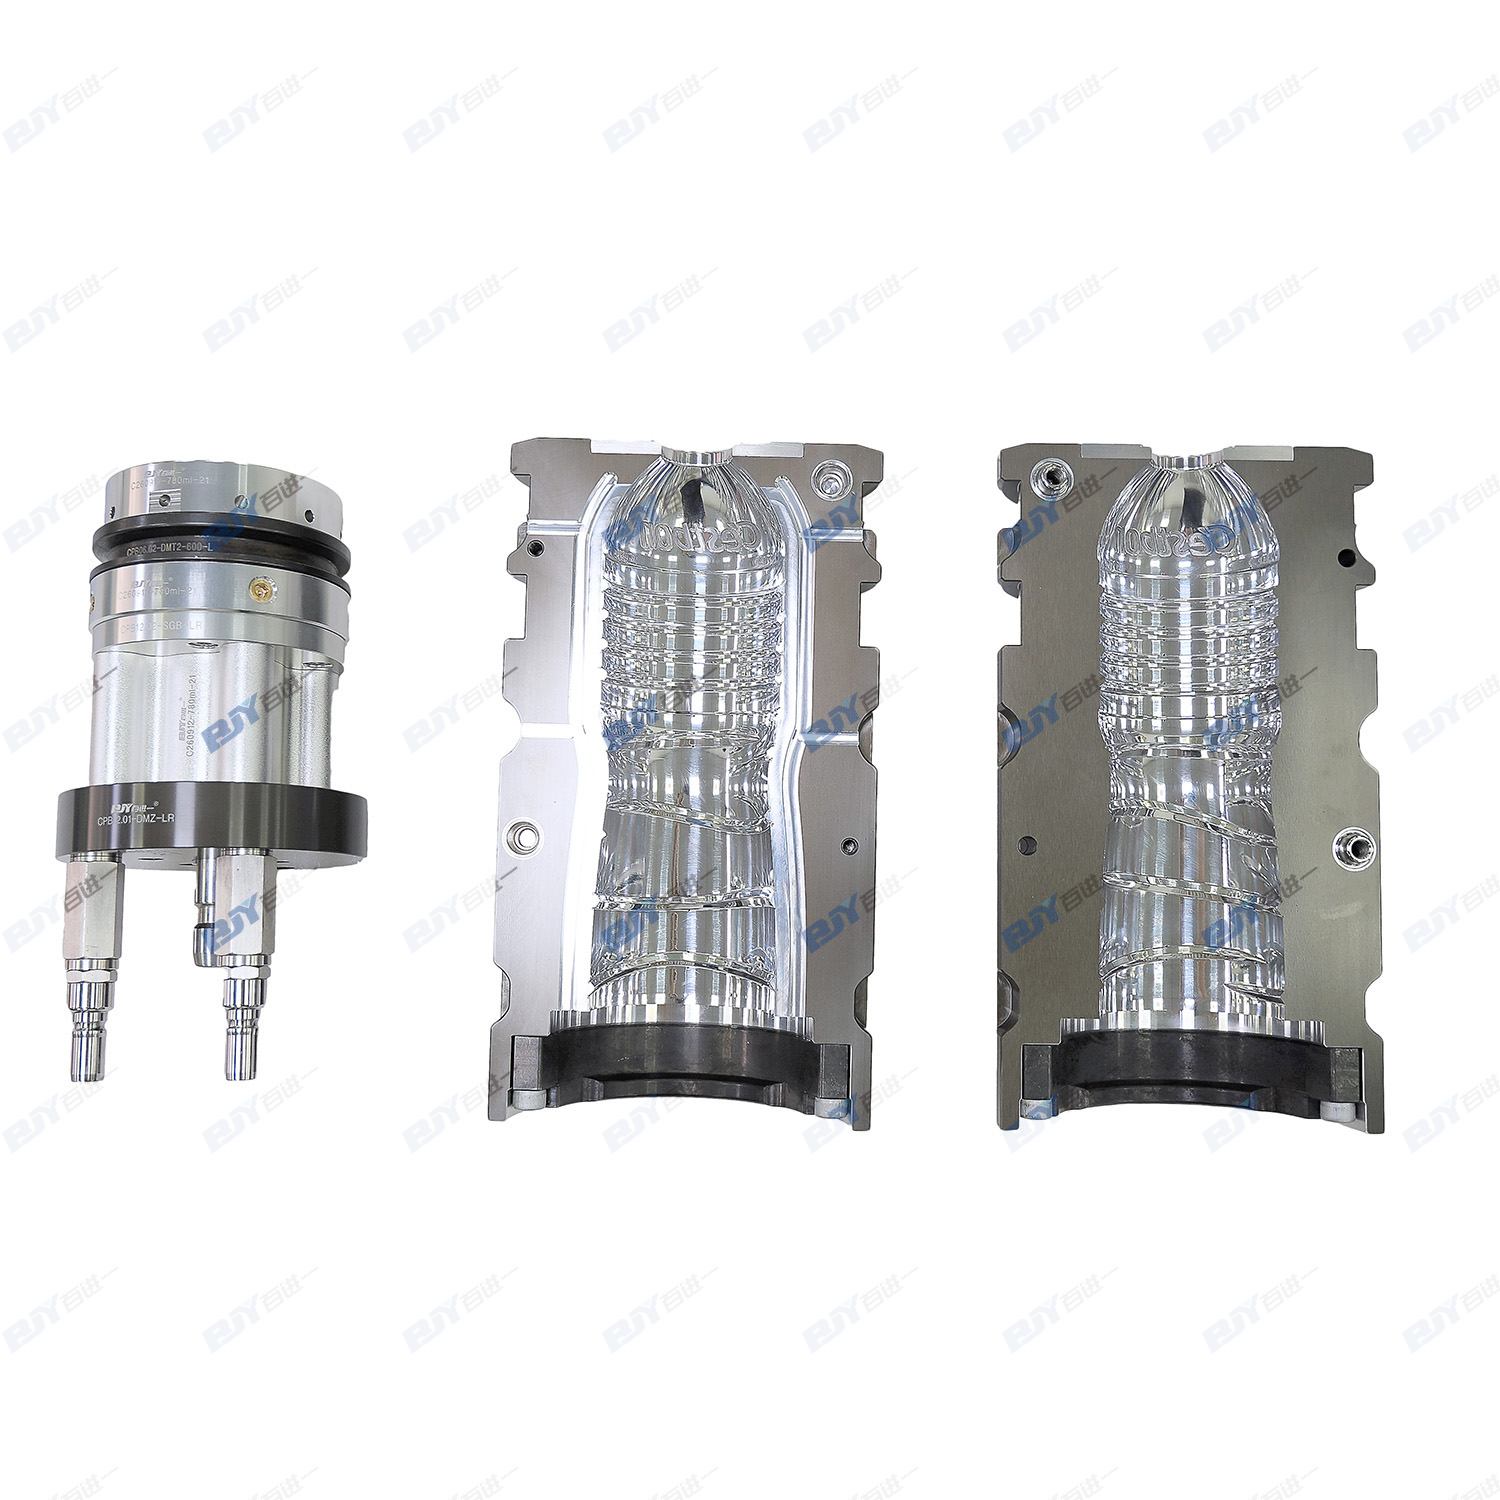
    BJY machines each core for a specific preform body. Molten PET runs into the space between the core and the cavity during the shot. The core seat holds the core in position while the shot happens. A water passes through the assembly and carries heat out of the mold.

    The core and the cavity form the preform wall together. The wall thickness at every point of the body is fixed by this pairing. At the blow stage the preform wall stretches to the bottle shape. An even core profile stretches evenly. The bottle then keeps a uniform wall.

  • Gap Controls Wall

    The distance between the core and the cavity sets the wall thickness. The drawing sets that gap. The machine holds it during production. Where the gap moves, the preform cools at uneven rates. Stress left in the wall then shows up in the blown bottle. A stressed preform resists the blow mold unevenly. The bottle comes out oval or thin-walled. Plants trace such failures back to the preform. The preform points back to the core.

    A preform body is not uniform by design: the shoulder needs extra material, and the bottom takes more stretch. The drawing gives each zone of the core its own tolerance for that reason.

    pet-mold-core-water-cooling-system.jpg
  • pet-preform-mold-core-working-surface.jpg

    Heat Out, Clean Part Out

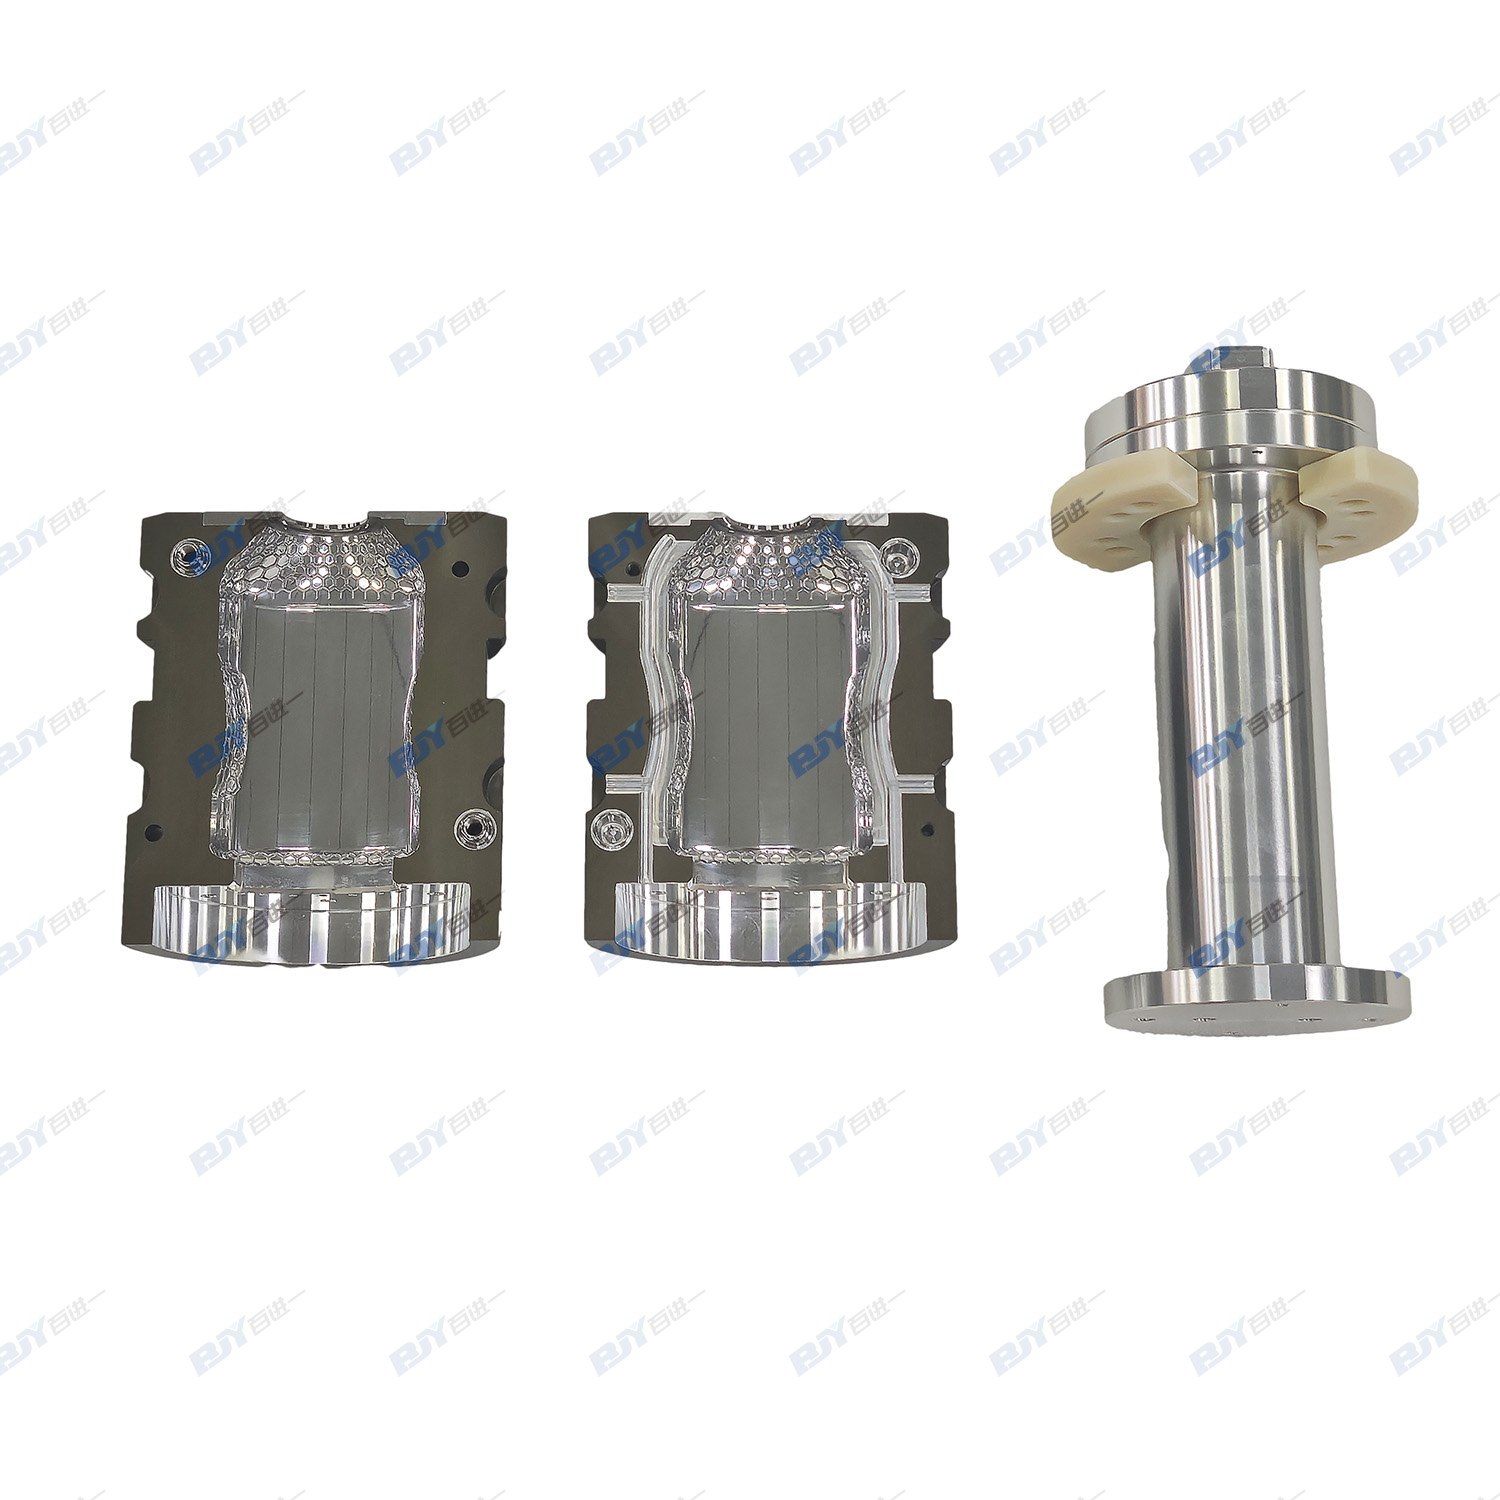
    The melt gives its heat to the steel around the core on every cycle. Cooling water in the mold half carries that heat away. A mirror-polished core surface lets the preform release without sticking. Flash at the parting line stays thin on that surface. BJY measures the core for concentricity after machining. The surface gets re-checked after hardening. The part that ships then matches the drawing the mold was built on.

    The water circuit gets pressure tested after the core is finished, and the plant keeps both results on one inspection sheet. Lot to lot, the preform weight the plant checks is a reading of this work.

Home
   
WhatsApp
Email
Contacts