Welcome to BJY
Product / PET Blowing Mold / BJY 2000L Blowing Mold
BJY 2000L Blowing Mold

BJY 2000L Blowing Mold

Product introduction

BJY supplies 2000ml blow mold cavities for PET bottle production. The cavity body is turned from aluminium and hard anodized on the outside only. The surface that forms the bottle is polished to mirror grade and stays uncoated. Each cavity is machined to the customer’s drawing and fits the blow molding machine already installed on their line.


Product specification


Field

Value

Product type

Blow mold cavity for PET bottles, 2000ml

Bottle volume

2000 ml (2 L)

Cavity body material

Aluminium

Forming surface finish

Polished to mirror grade, no anodizing on this face

Outer surface treatment

Hard anodizing, outer face only

Machine fit

Machined to the customer’s drawing, fits the machine they already run

The installation issues on the bottle blowing production line are rarely caused by the molds themselves, but rather arise from the contact areas between the molds and the machine.There are several measurable aspects of these contact points: the mold installation slots, the total height of the mold, the depth of the pressing block position, and the alignment of the two sides of the mold, etc. These aspects were all determined by BJY before confirming the design and production of the mold. Before packing the molds, we will check the total height based on the drawings. We will use simple molds for prototyping or test molds to verify the capacity, and then install them on the bottle blowing machine for inspection.
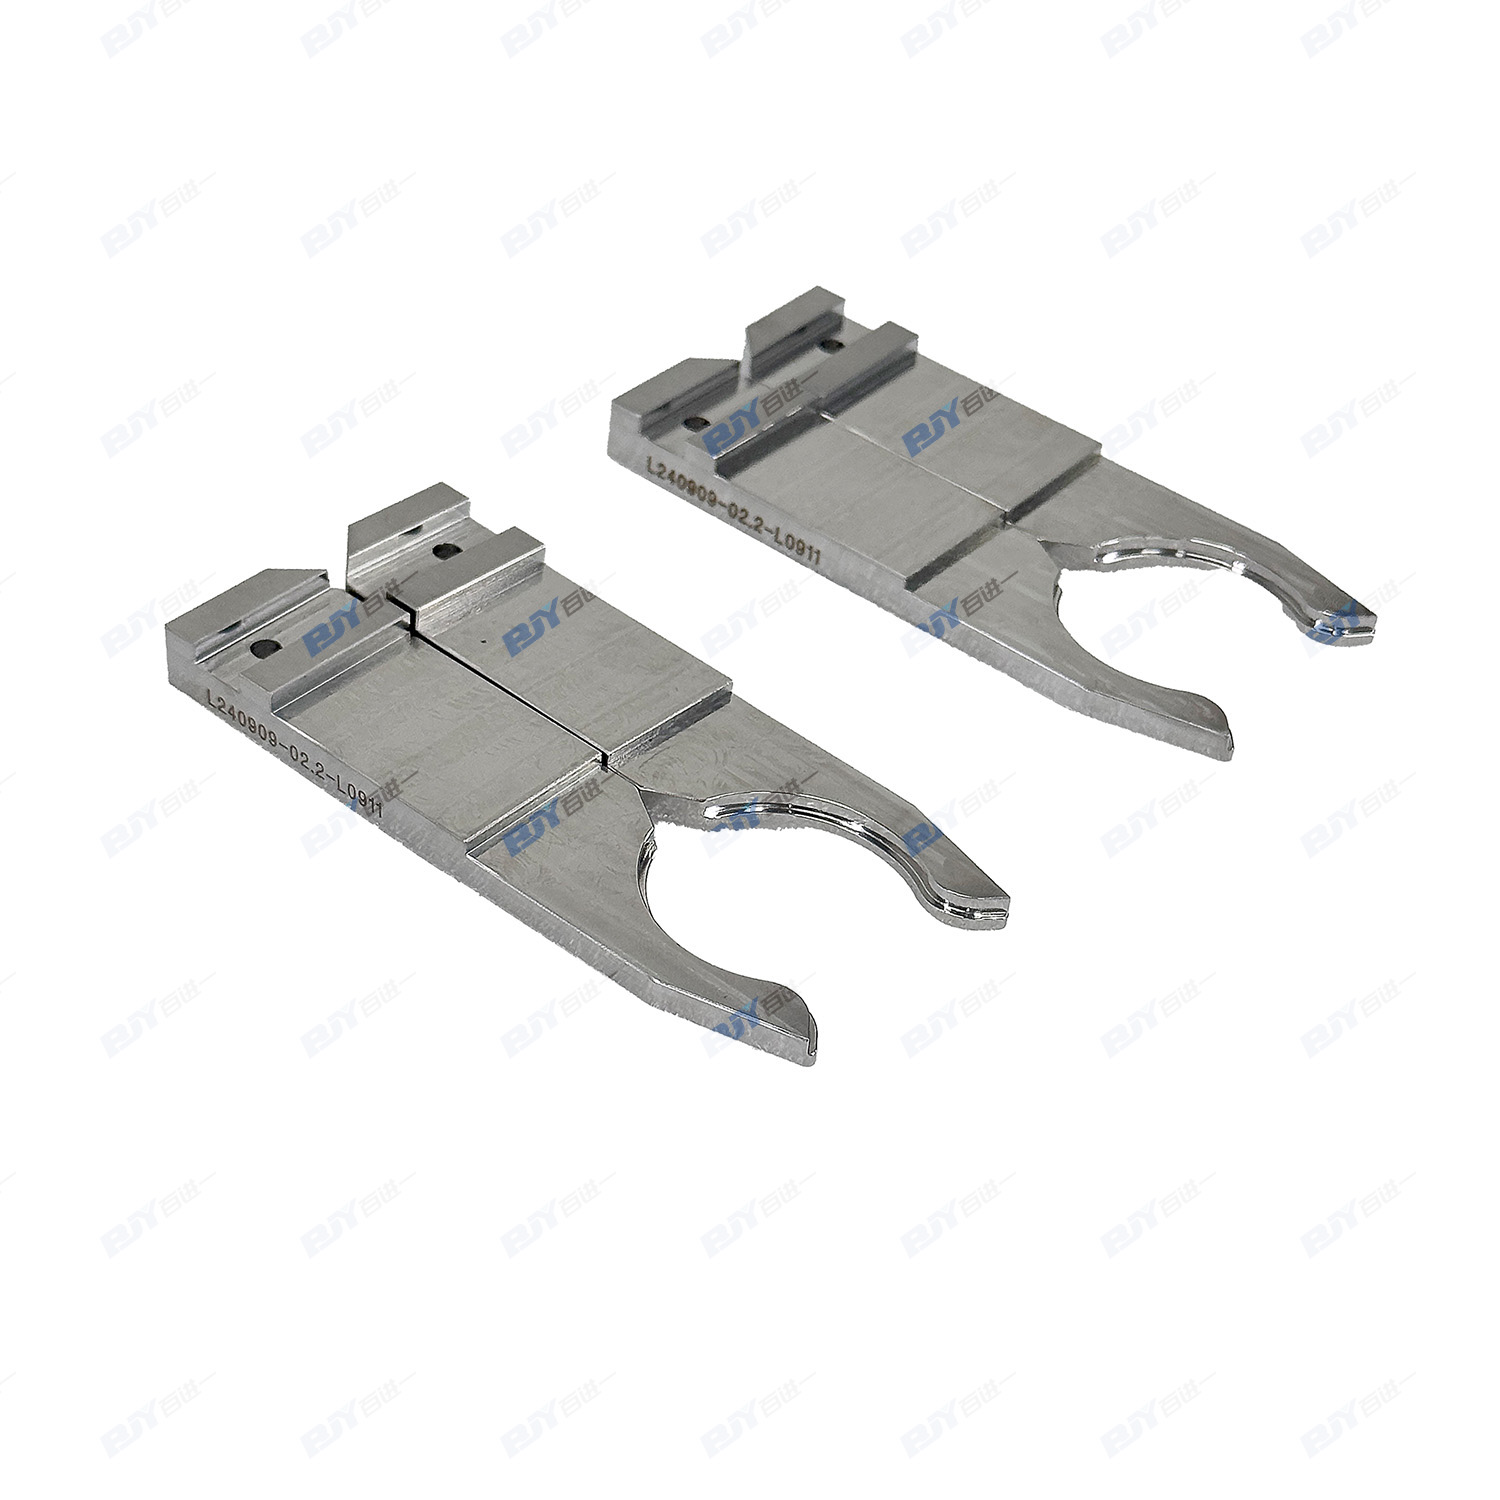
  • precision-2000ml-pet-blow-mold.jpg

    Height is the reference dimension, not an adjustment item


    Before packing the molds, BJY will check the total height based on the drawings. The two halves of the cavity must remain on the same horizontal plane. If the two halves of the mold are not level, the parting line will not close uniformly, and the shape and thickness of the bottle will change along the circumference of the bottle body. The pressure setting cannot compensate for this problem because the position of the mold and the machine has already been fixed before the production cycle begins. When the factory reports that the bottle shape changes between different shifts, we will first inquire about the situation of the mold mounting base and the mating surface, and then check the pressure setting in this order to troubleshoot.

  • Clearance needs to be measured at working temperature


    When the aluminum material is heated, it expands. Therefore, the clearance set on the cold mold will gradually decrease after the production starts. When measuring, the mold should reach the working temperature and use a feeler gauge as the measurement benchmark. The feeler gauge should be able to insert with slight resistance. If there is no sense of contact when inserting the feeler gauge, it indicates that the mold clearance is too large, and the parting line will have overflow. If the feeler gauge cannot be inserted, it means that the locking mechanism is bearing a load beyond its design requirements. During adjustment, the master of BJY will slightly adjust the limit screw, and recheck with the feeler gauge after each adjustment step, because a large rotation at once may cause the mounting base to move beyond the range that the feeler gauge can reflect.

    bjy-2l-pet-bottle-mold.jpg
  • aluminium-blow-mold-cavity-bjy.jpg

    Storage method determines the mold change time


    When the molds are stored, the two halves remain locked, and the mating surface can be protected.If the two halves of the mold are placed loosely, they are prone to being damaged by external impacts, resulting in internal forming defects. During the next mold replacement process, an additional repair step will be required instead of directly starting production. The fixed storage positions, protective partitions and horizontal storage racks provided in the tool room equipped in the factory can help reduce this risk.

Home
   
WhatsApp
Email
Contacts